High Altitude Vacuum Testing of Electrical Connectors and Components
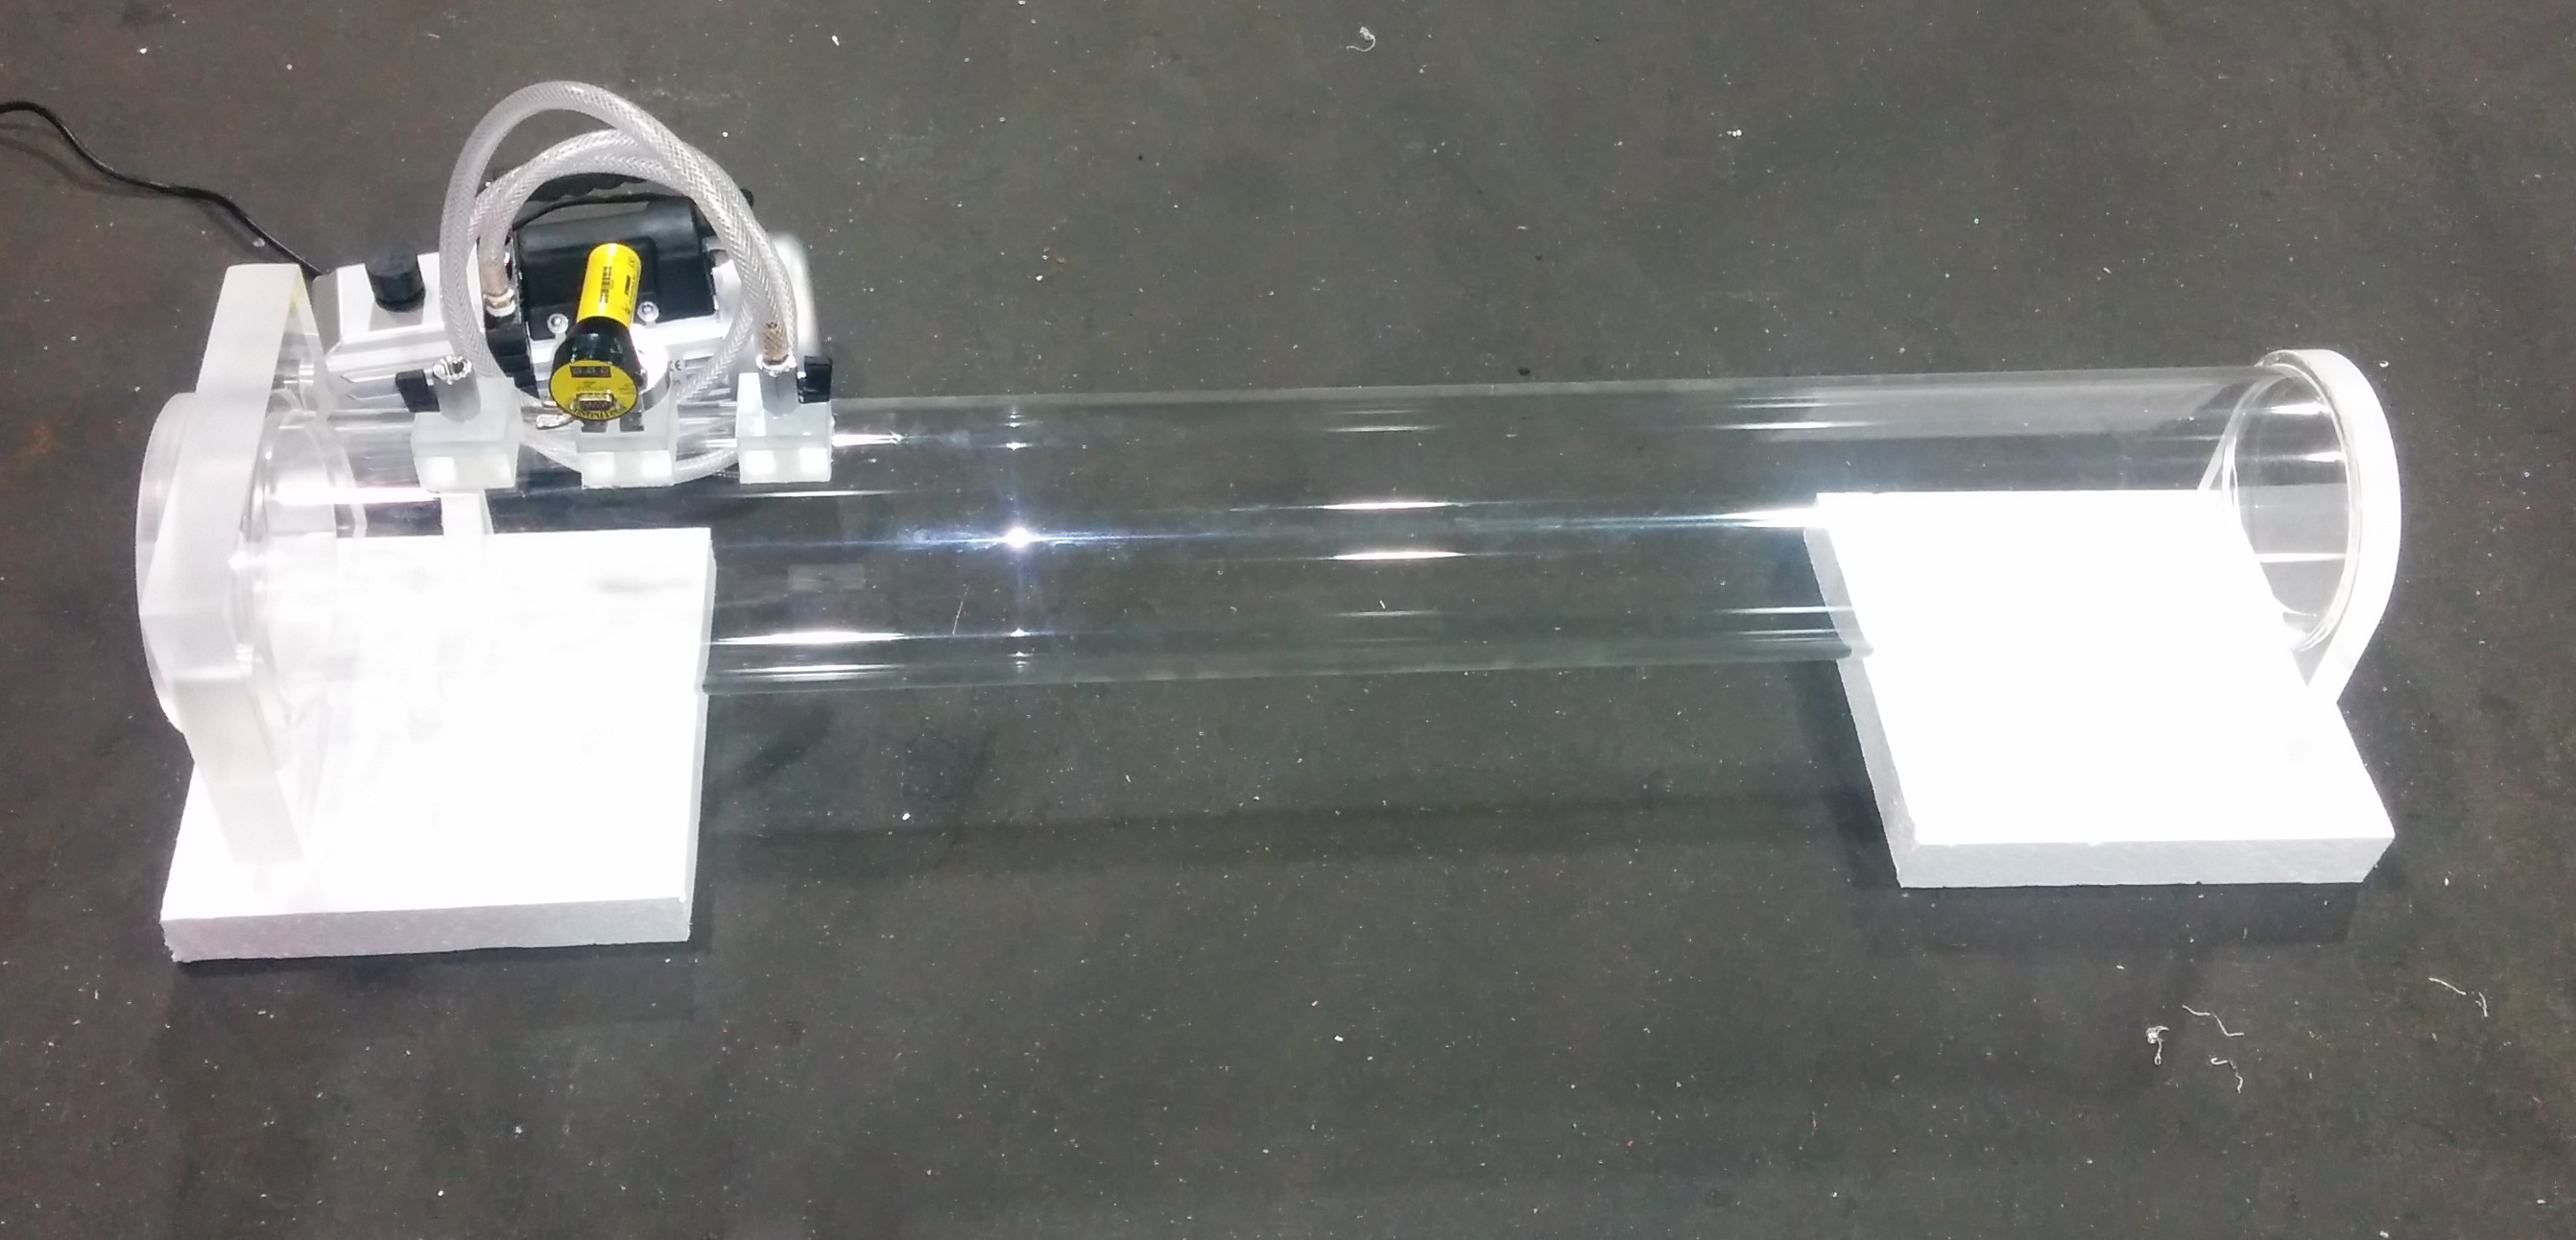
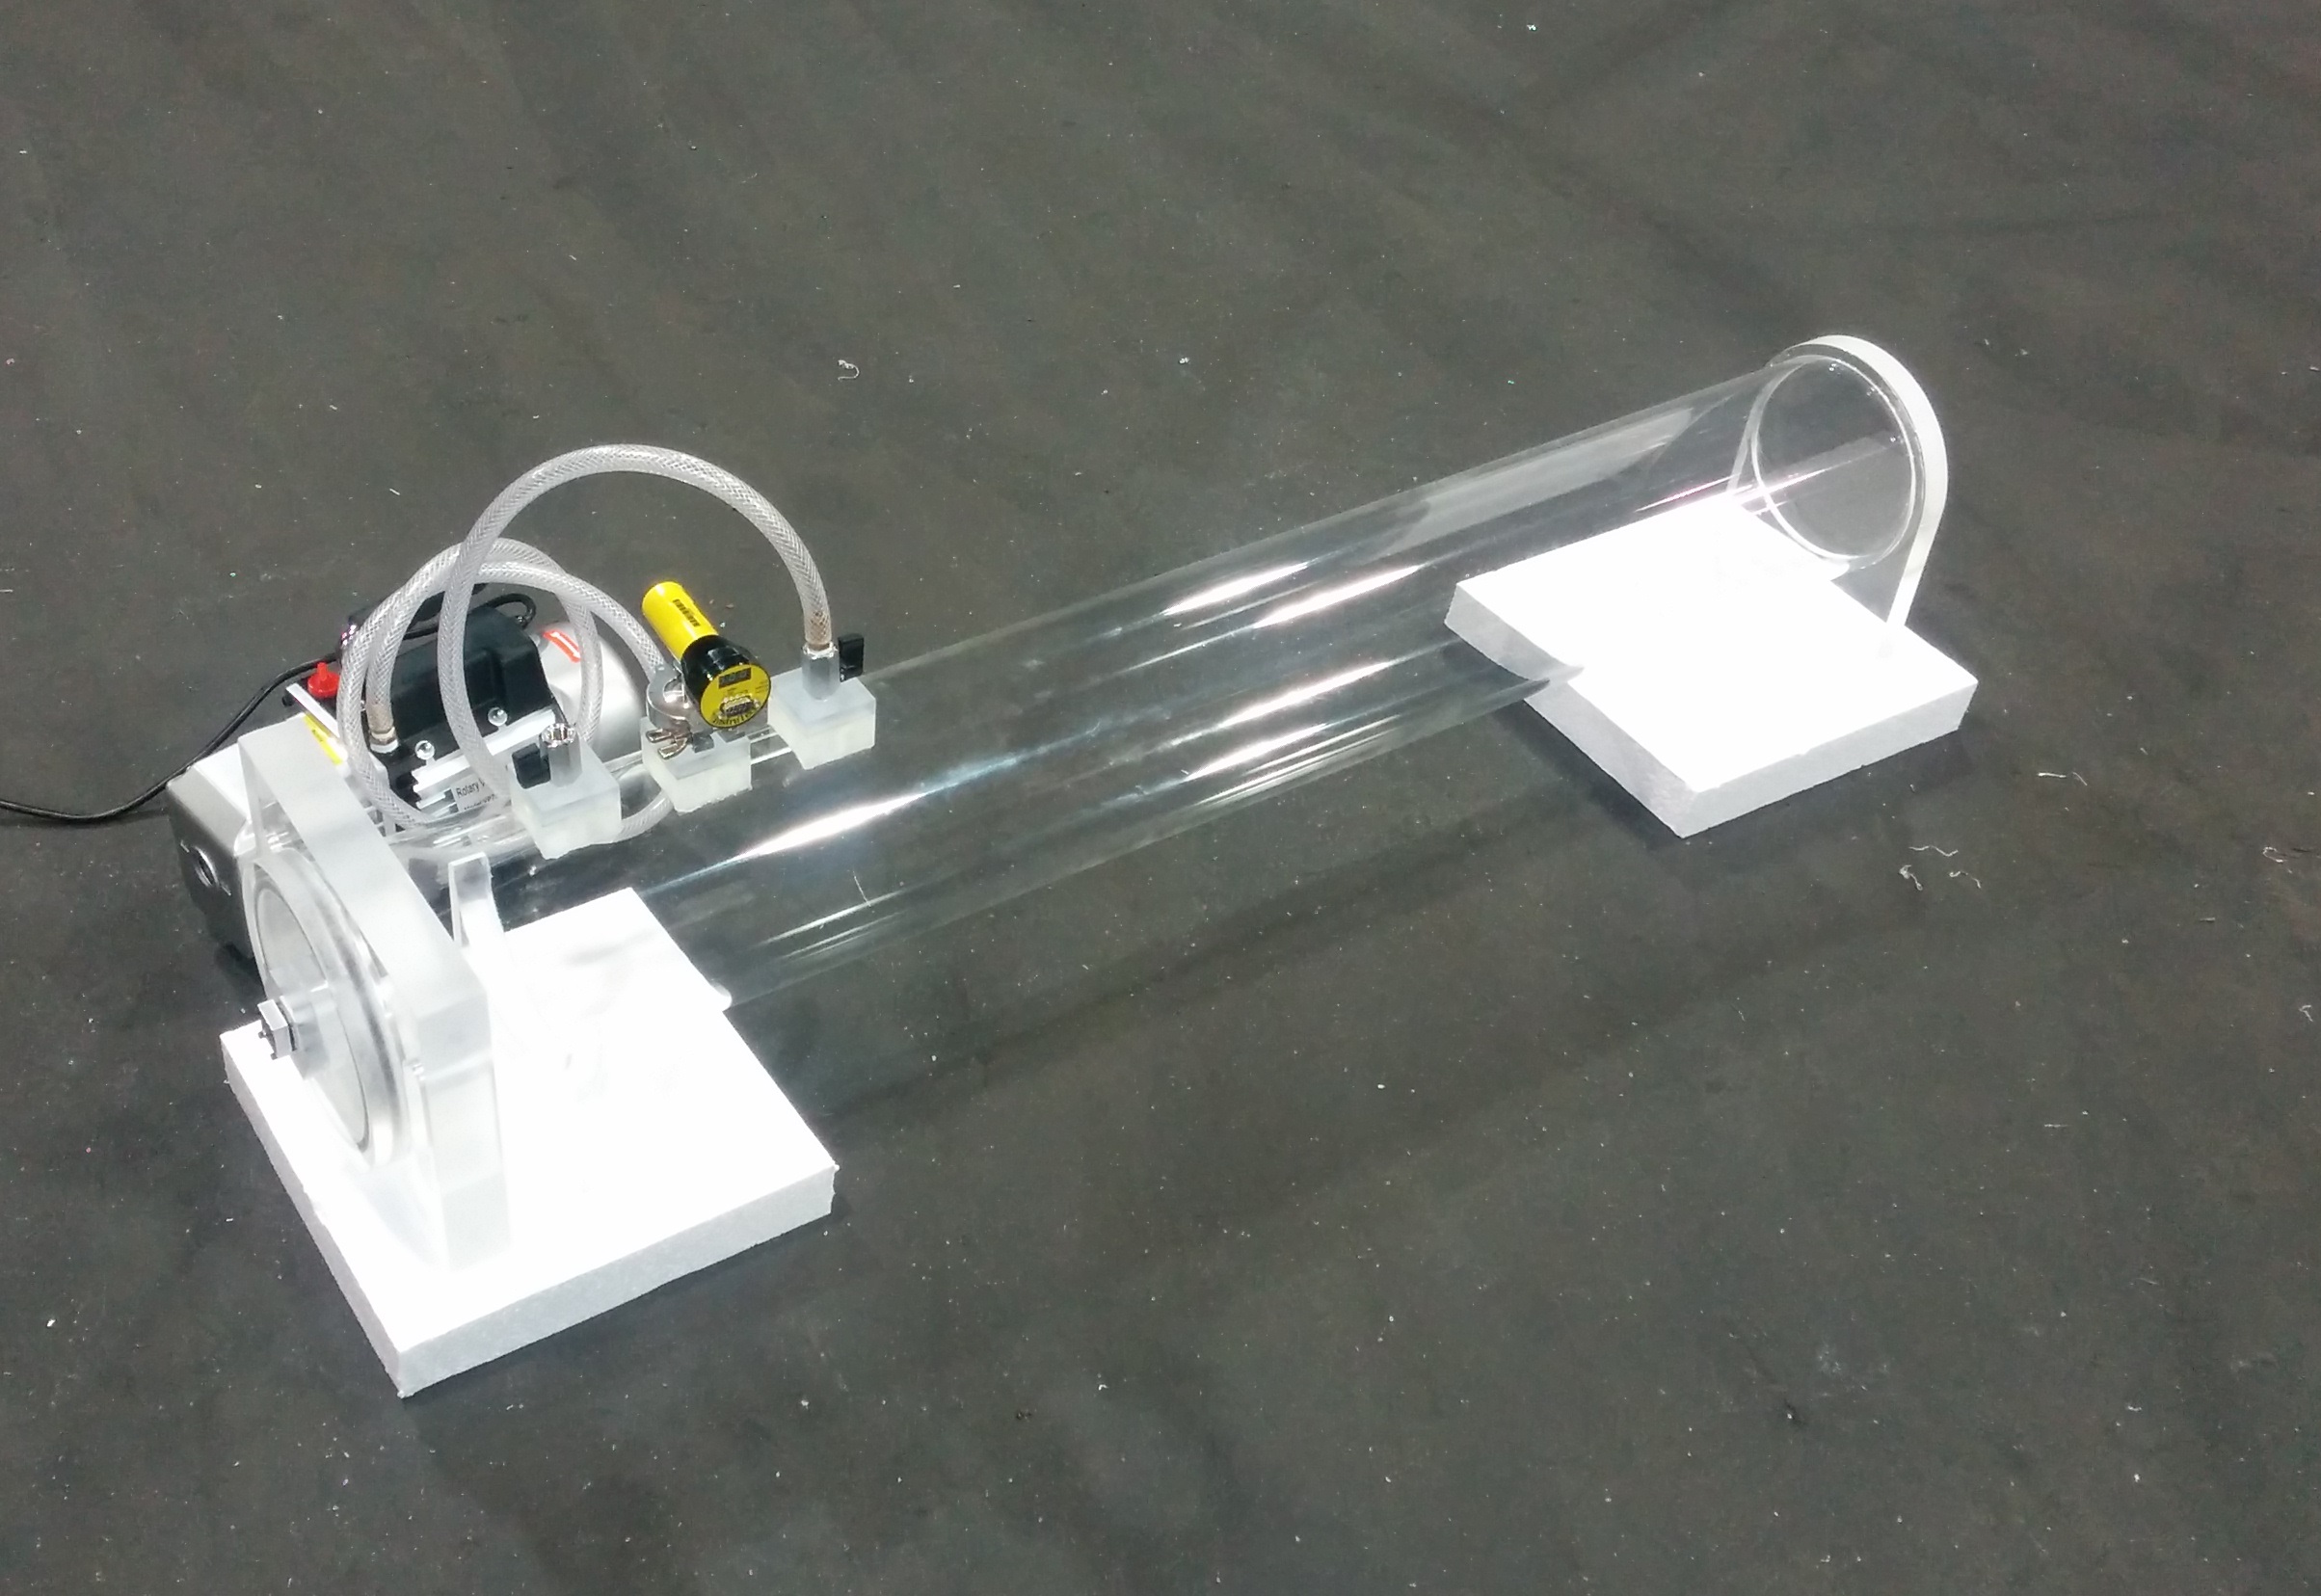
high altitude test chamber of electrical components
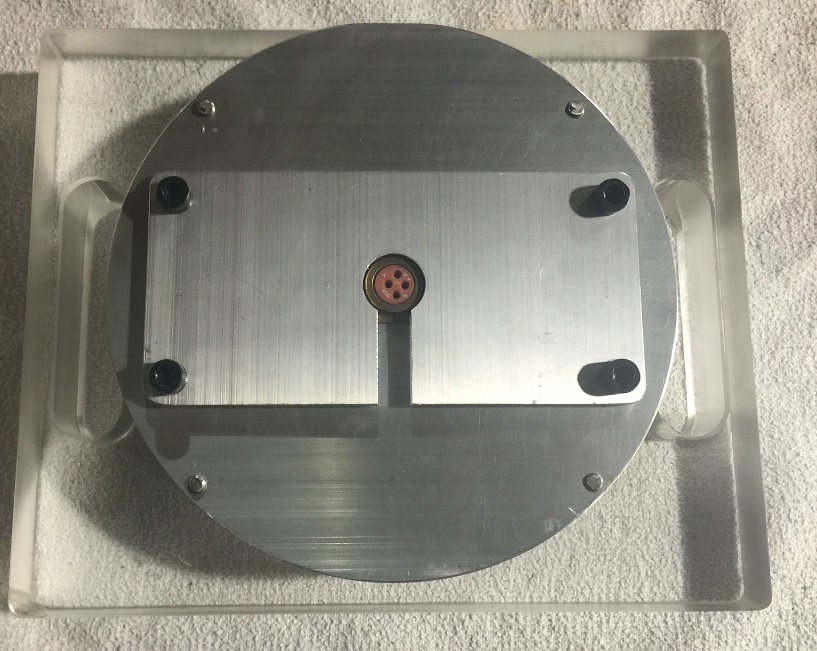
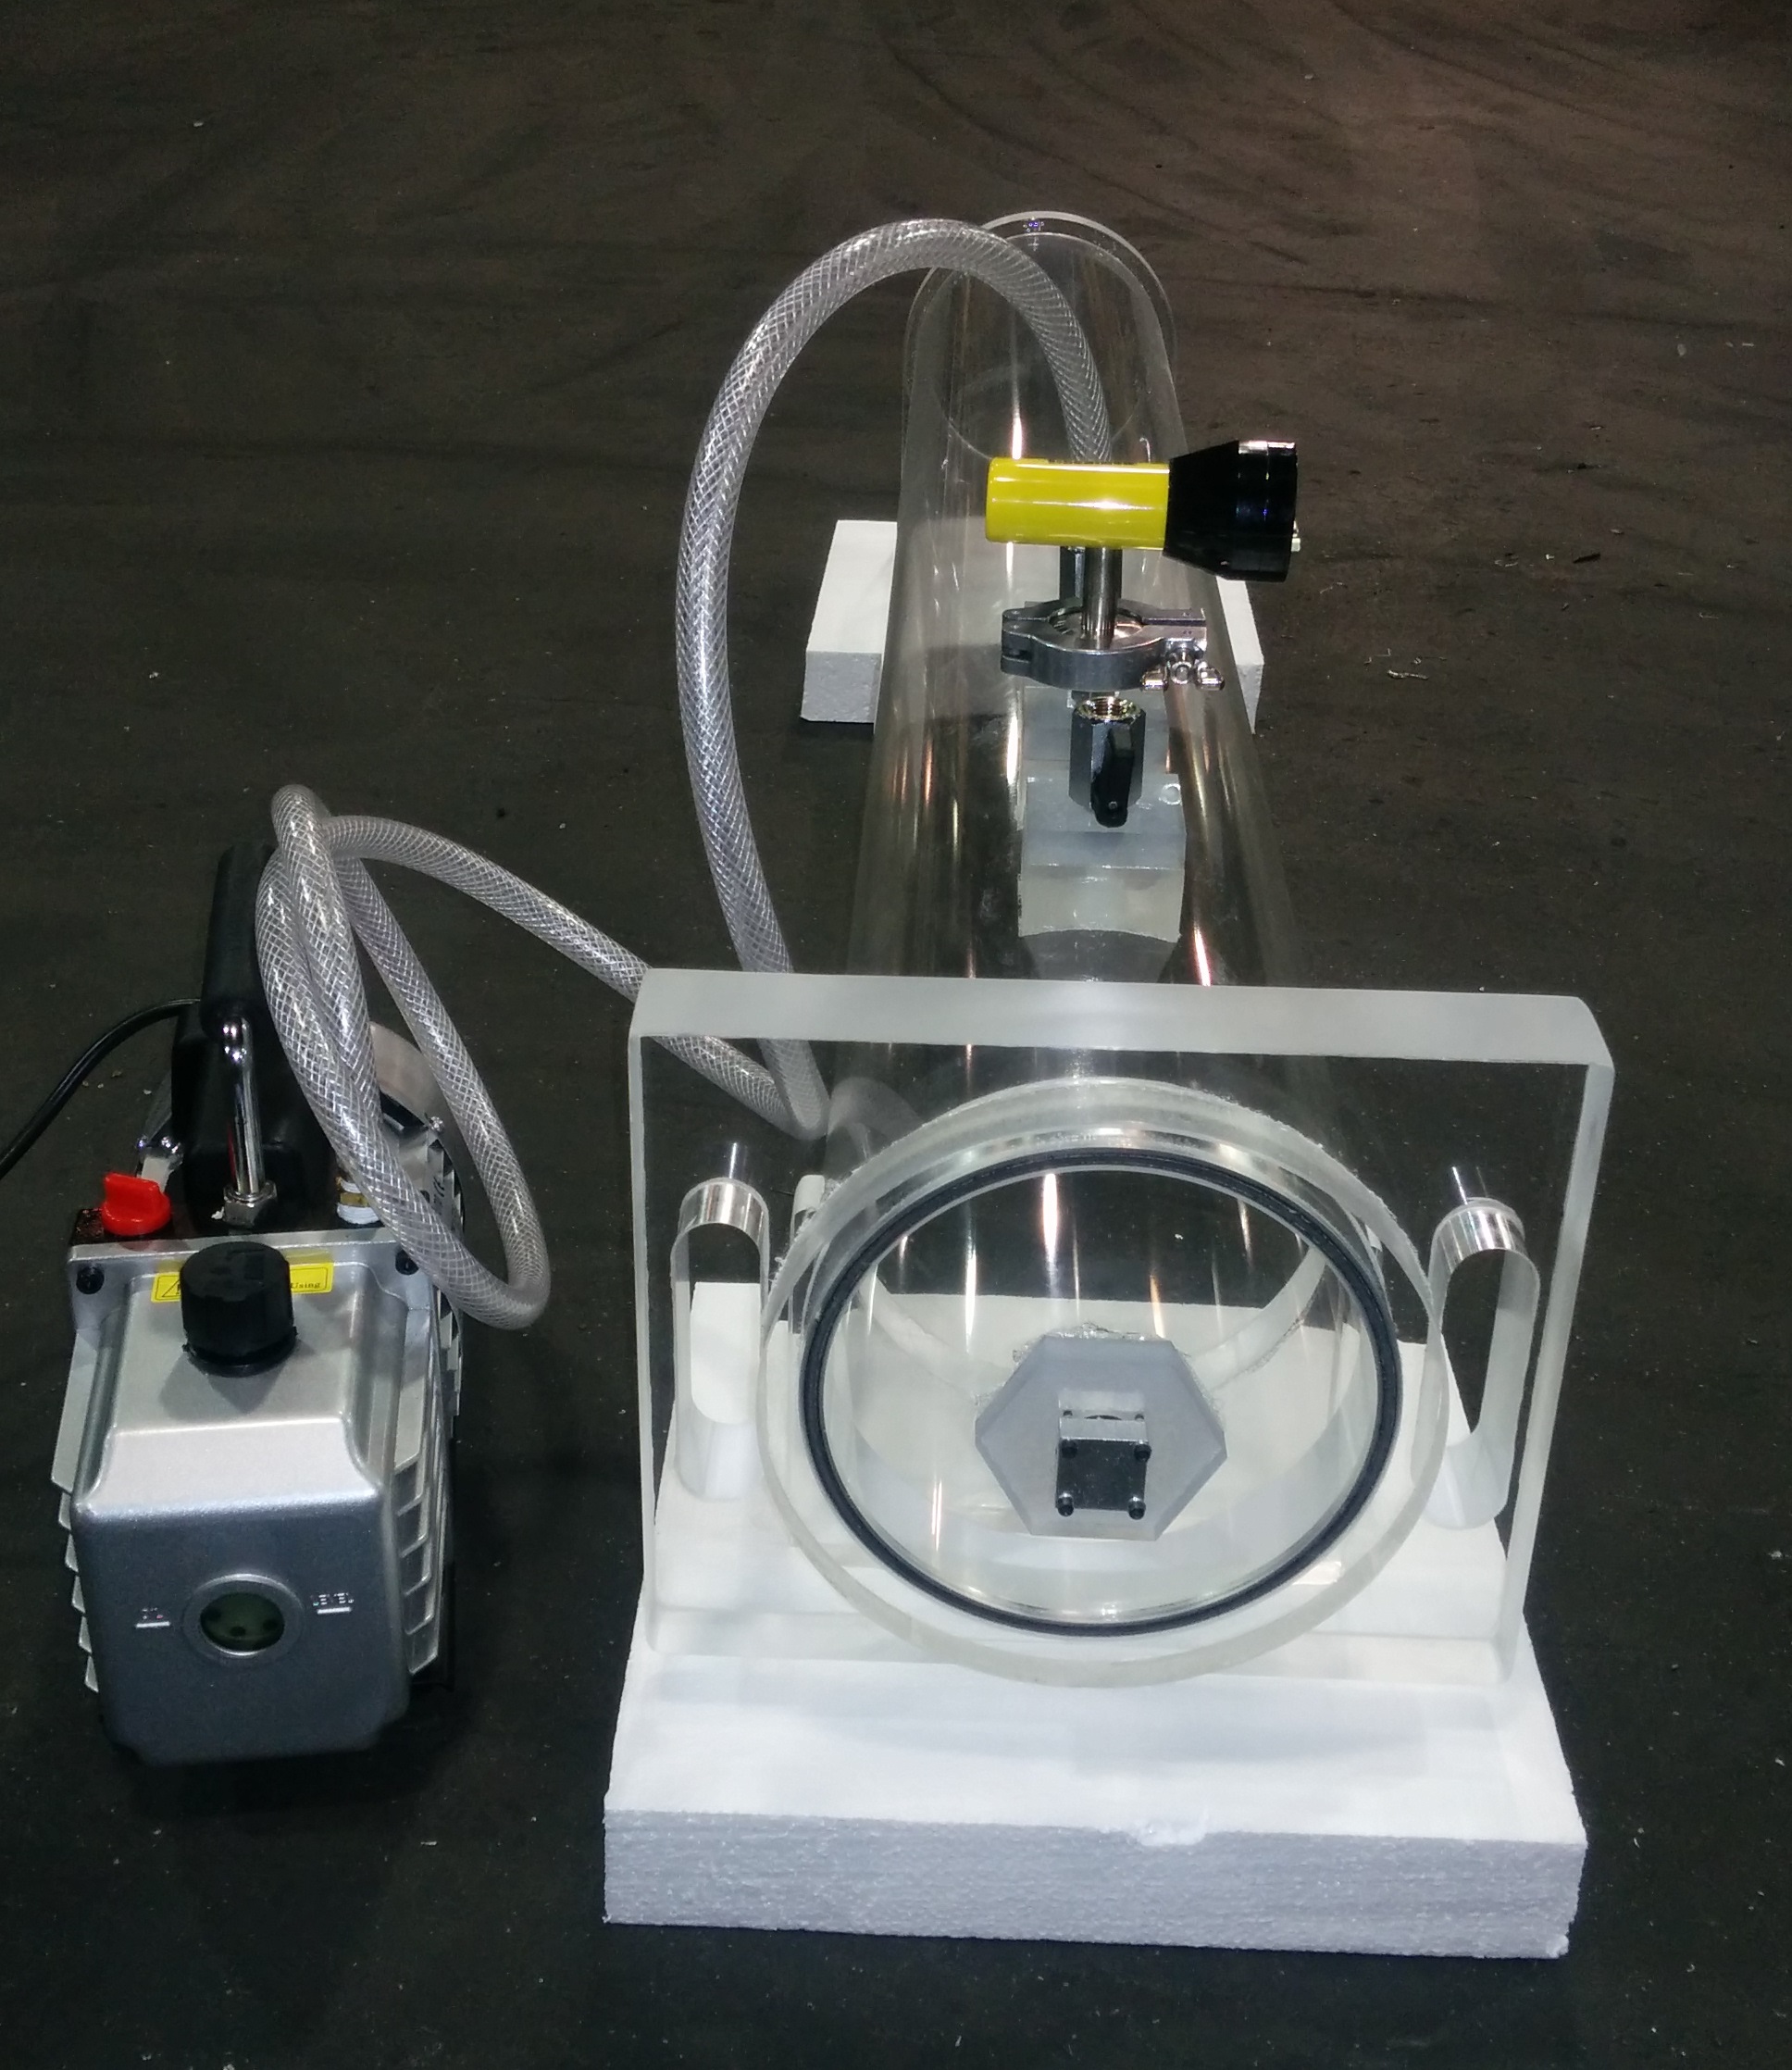
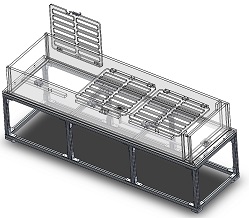
Rear view of the Custom Vacuum Extrusion Chamber
This was an interesting project where one of our customers needed to test wires up to 44 inches long within a high altitude simulation environment. In addition to testing wires, several other electric connectors required altitude testing as well. The altitude requirements were 100,000 feet (30.510 km) which corresponds to 8.36 Torr - a piece of cake when it comes to the vacuum requirements of our chambers.

We would like to take a moment and bash our competitors on this one and point out where they went wrong: Our competitors have sales people and not engineers communicate with their customers when it comes to understanding customers design requirements. This leads to suggesting over-engineered solutions of humongous projects, prices, and lead times. When this customers came to us to, our question to them was simple: "What exactly are you trying to accomplish and what are the exact dimensions of the part you were testing?" This enabled us suggest a chamber which was 52 inch long and about 6 inch in diameter with a custom designed lid. Our quote blew our competitors away because 1. their sales staff had no idea what the customers goals were and 2. they were over-engineering, hence overcomplicating a simple problem.

What you see here is a:

1. custom vacuum chamber which allows for plenty of space for electronic wires and widgets to be tested at high altitude.

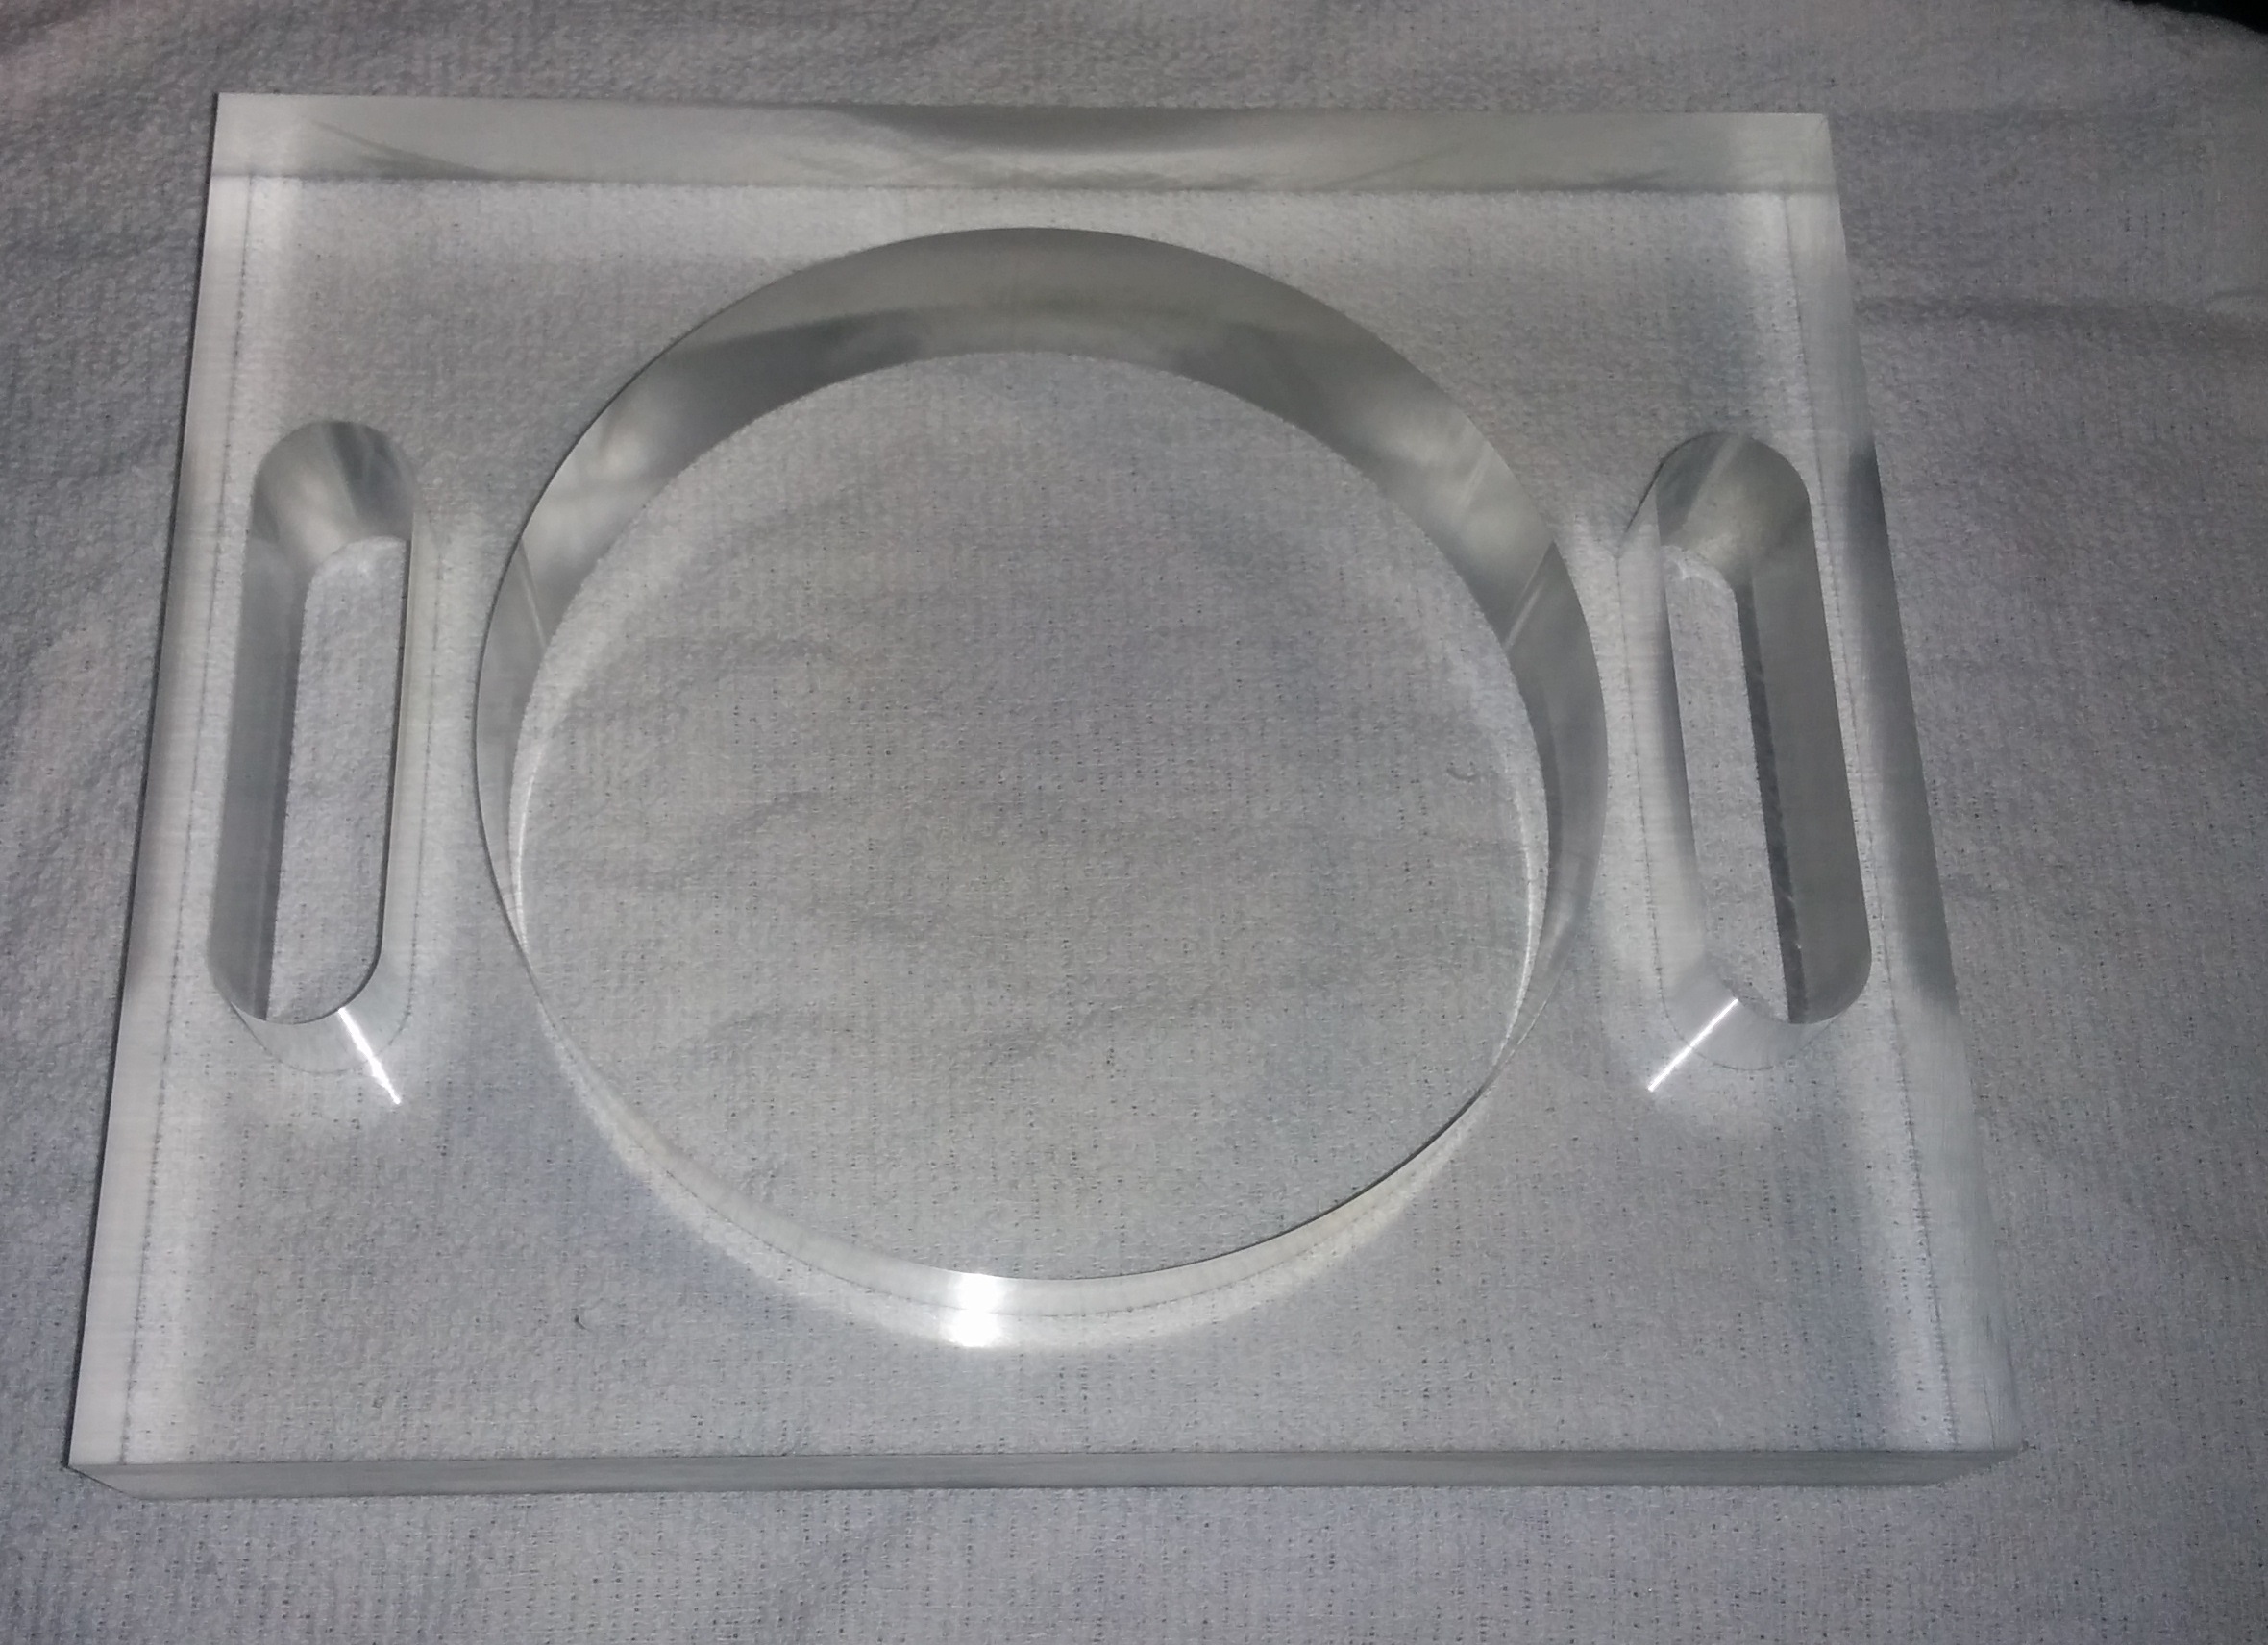
2. A custom design vacuum chamber Lid which allows for flexible electronic connector changes enabling fast and reliable high altitude electronic equipment testing.

Some of our Popular Items

We are an Engineering Excellence Company. Check out some of our other items we carry that you can combine/integrate with your systems or projects.
Internal Pressurization ASTM F2096 Leak Testing Systems
Internal Pressurization (ASTM F2096) Leak Testing Systems are instruments that are used during the Quality Control process to discover leaks in sealed packages. As opposed to the vacuum bubble leak test, where the specimen is subjected to a vacuum, the internal pressurization integrity test creates a pressure difference and drives the air through a leak by internally pressurizing the specimen. Our Internal Pressurization Leak Testing Systems are designed and built to conform to the ASTM F2096 Protocol Standard.
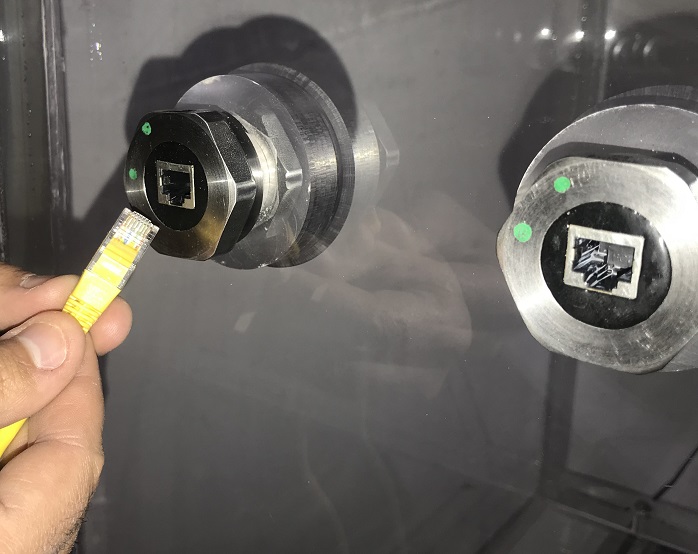
Ethernet Vacuum Feedthroughs
Ethernet Vacuum Feedthroughs are Vacuum Rated Ethernet connectors that enable you to run ethernet cables into your vacuum chamber. Simply connect your ethernet connector to the outside of the vacuum chamber and another ethernet cord from the inside and run it into your part present inside your vacuum chamber.
Our Work: Altitude Testing in a Vacuum Chamber
It is not a secret that you can simulate a certain altitude in a vacuum chamber. The good thing about Acrylic Vacuum Chambers is not only that you can simulate an altitude of up to 250,000 feet, you can also fully view your test specimen during your testing operation.
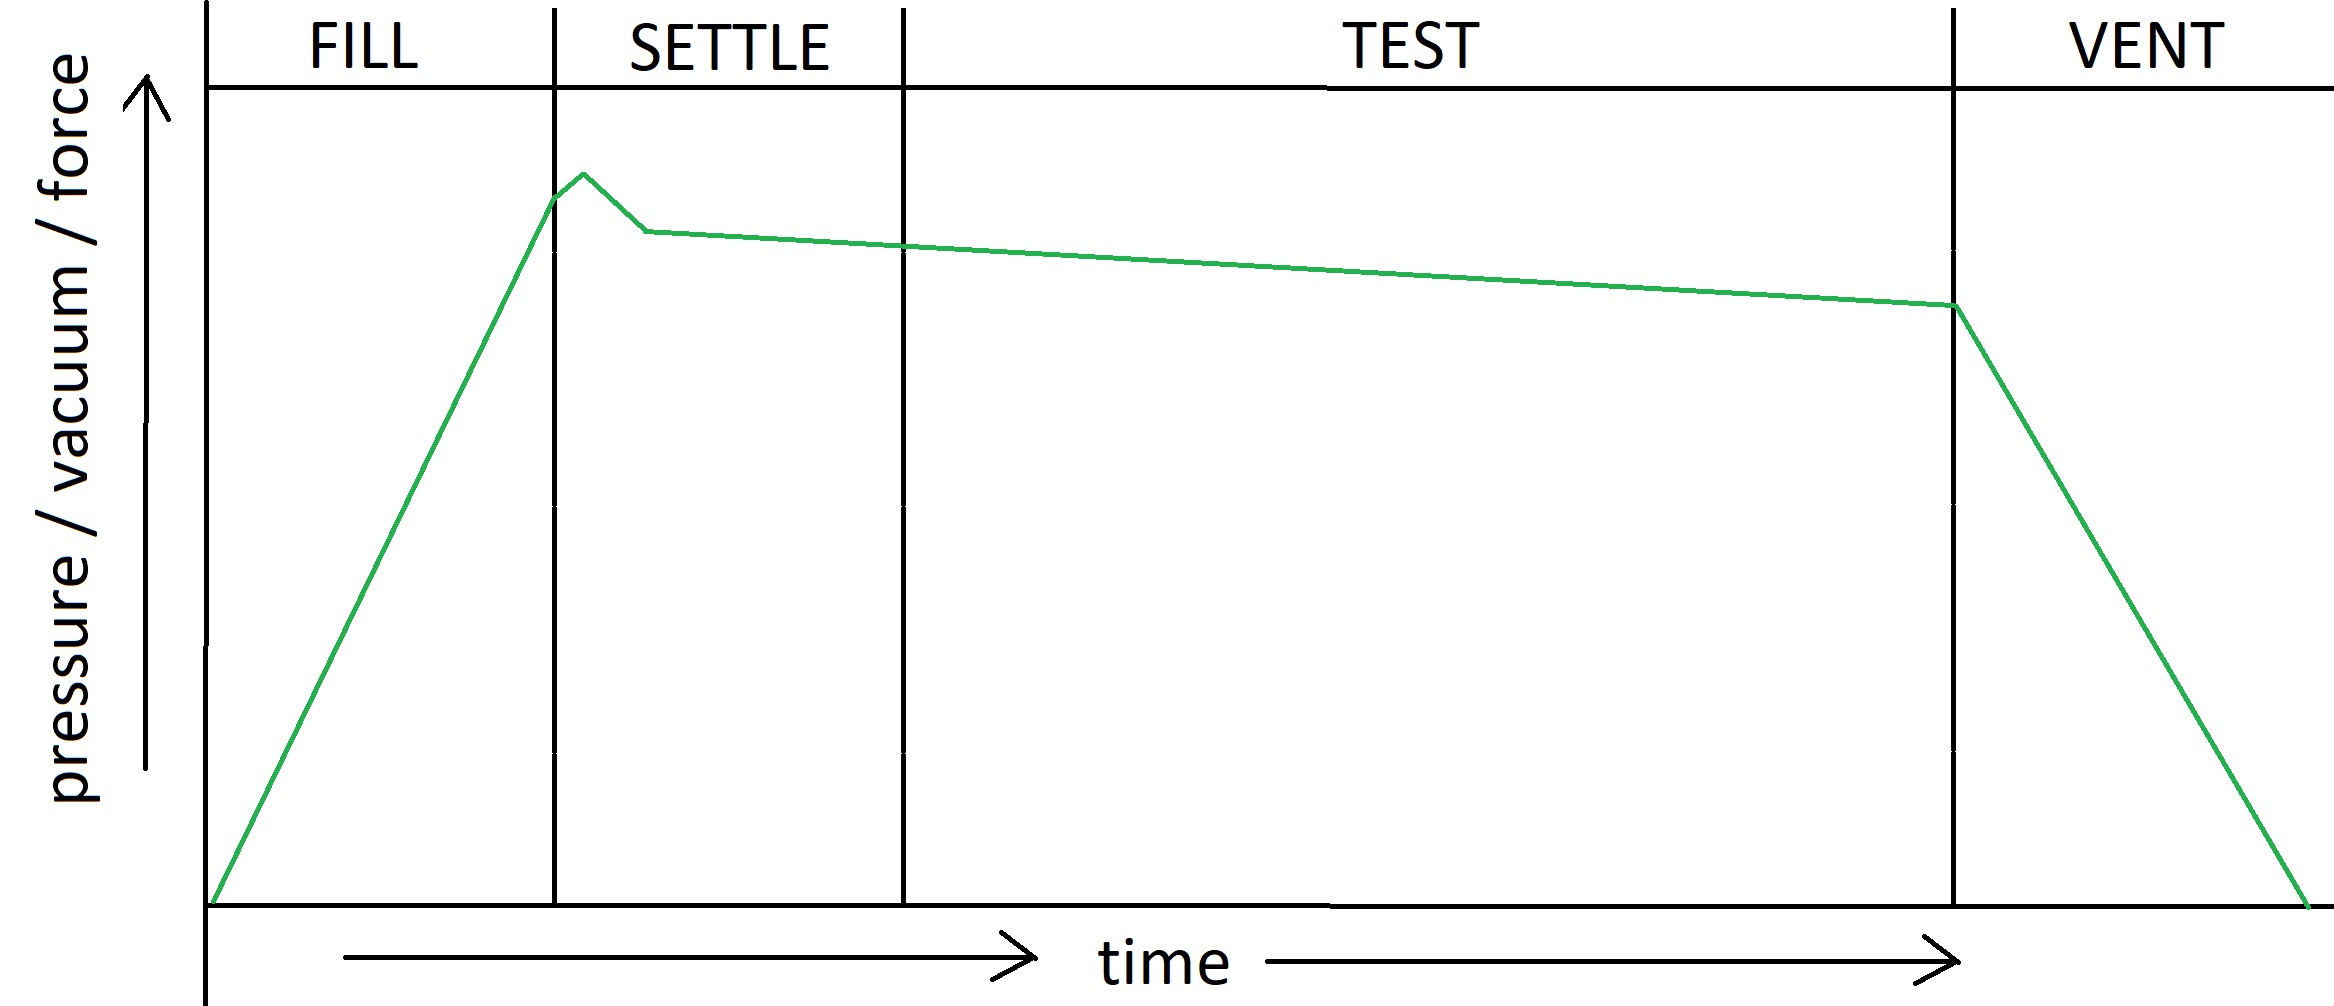
Related Articles: Anatomy of the Pressure Decay, Vacuum Decay, and Force Decay Curve
How do you know that you have a good part during your leak test? In order to understand your leak test, you must first understand the Test Decay Curve and what it tells you about your test specimen. There is a certain way that a test specimen behaves during the leak test.